What Is Contract Manufacturing? Understanding the Process and Benefits
What is contract manufacturing, in one paragraph?
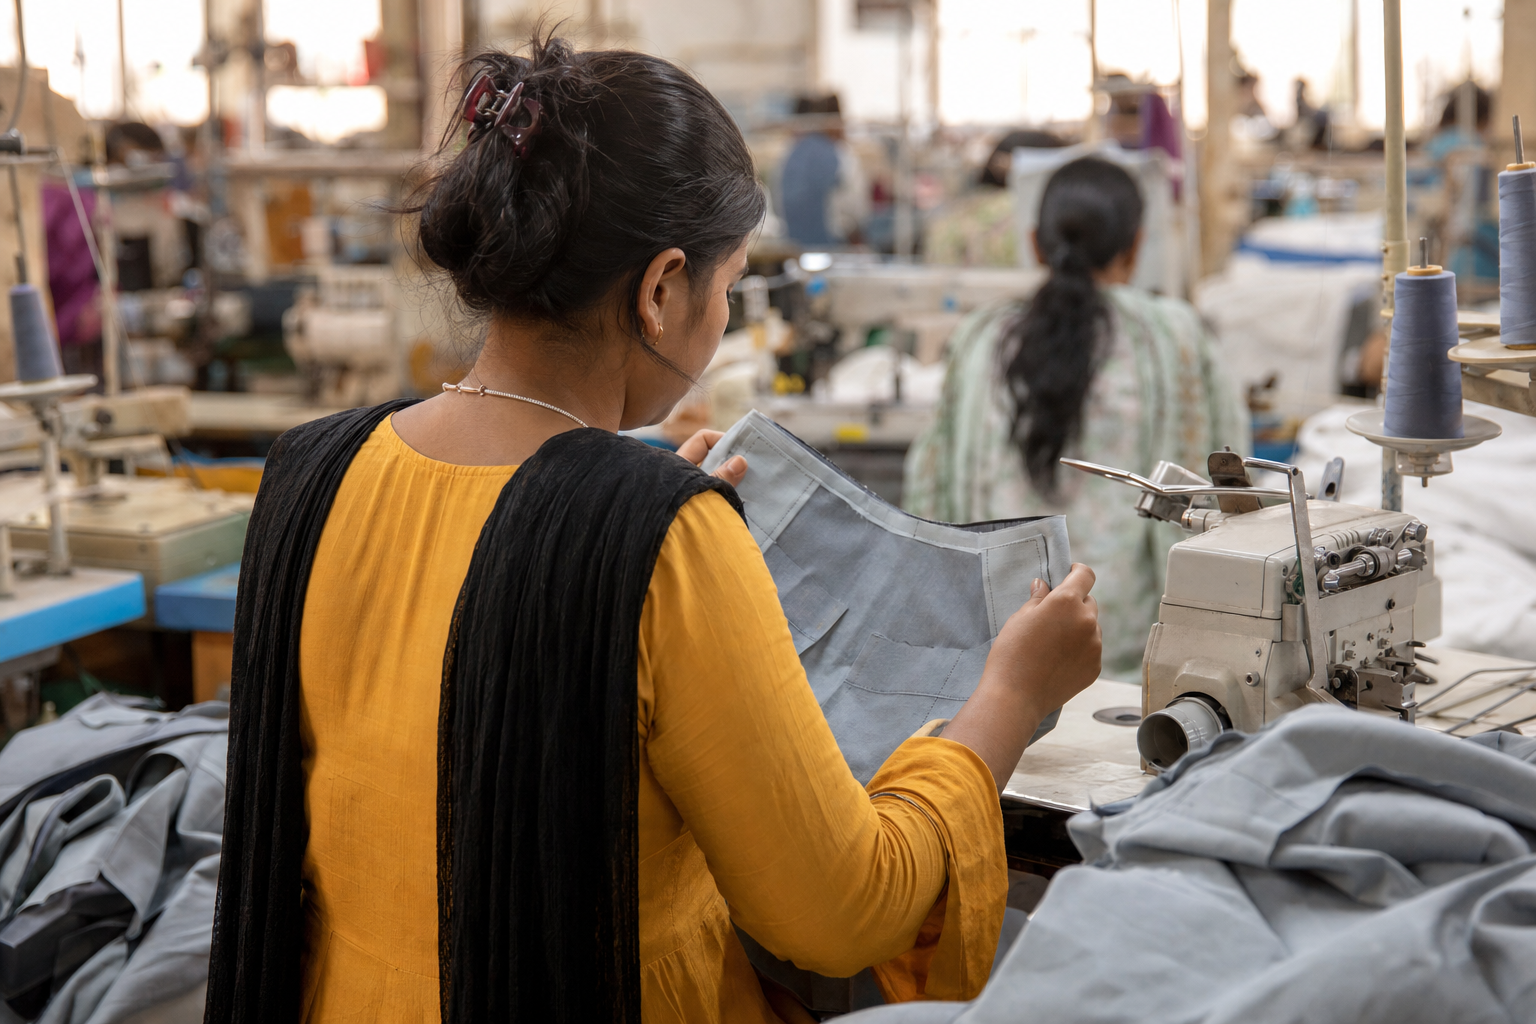
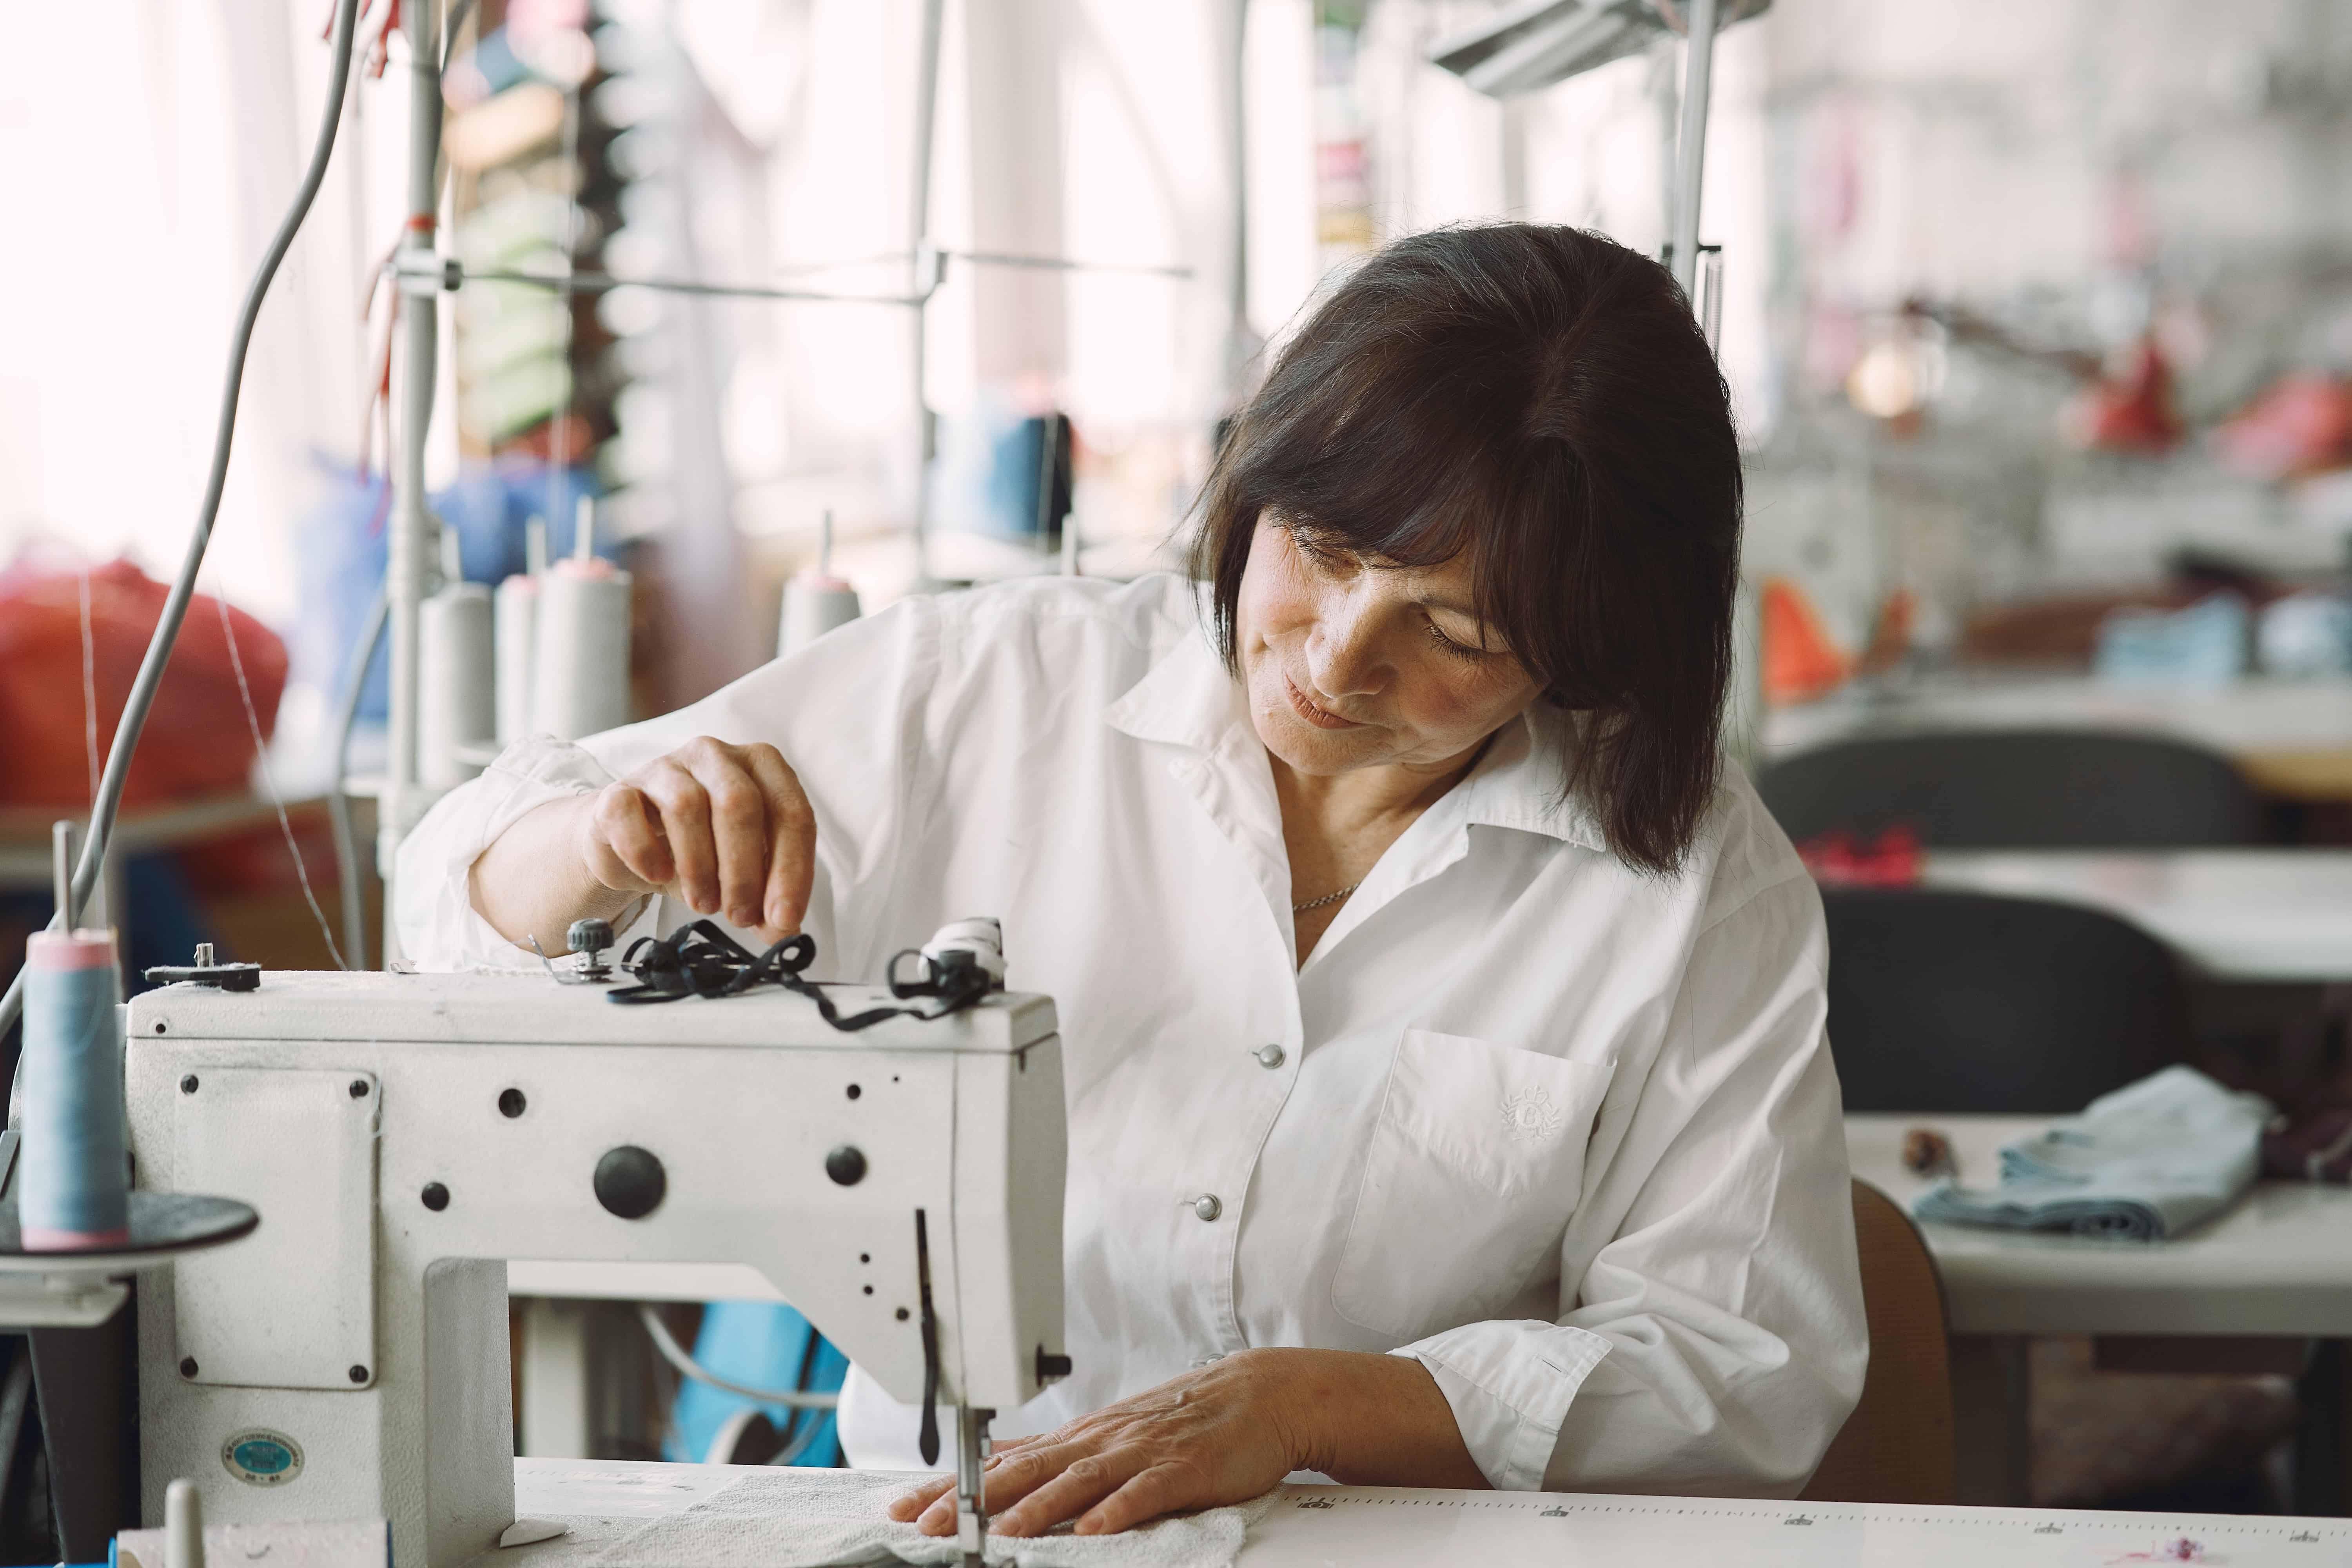
Contract manufacturing is a sourcing arrangement in which a brand delegates the physical production of a product, or a component of a product, to an external factory called a contract manufacturer. The brand owns the design, the tech pack, the materials specification, and the intellectual property. The factory owns the machines, the labor, and the production floor. The contract defines the price per unit, the lead time, the quality tolerances, and who carries the risk when something slips. In apparel, this is the dominant model: the overwhelming majority of brands in the $5M to $100M range do not own cut-and-sew capacity.
From the go-lives I have run this year, the pattern is consistent: the brands that treat contract manufacturing as a procurement decision alone end up firefighting. The brands that treat it as an operations decision, with product data, production tracking, and inbound inspection built around it, hit their ship dates. That distinction maps directly onto the second of the 6 Breakpoints of Apparel Operations, where production and supply execution drift from the plan.
How does contract manufacturing actually work, step by step?
Contract manufacturing has become the default for brands that want to expand production without the capex of a factory, the hiring of machinists, or the training burden of specialized staff. It is a form of outsourced manufacturing, and it moves through a predictable sequence.
Step 1: Identifying the need to outsource
The first step is naming why you are outsourcing. The honest answer is usually one of three things: you do not have the capital for in-house production, you do not have the specialized expertise (for example, cut-and-sew denim, performance knits, or technical outerwear), or you want to keep internal headcount focused on design, merchandising, and brand. Write the reason down. It will shape the type of factory you look for.
Step 2: Searching for a contract manufacturer
Once the decision is made, the next step is finding factories capable of handling the full production run from fabric intake to finished-goods pack-out.
- Research potential manufacturers that align with your product category and quality standards.
- Evaluate technical capabilities, production capacity, and compliance with safety and environmental regulations.
- Assess financial stability and reputation to ensure the partnership survives a bad season.
Step 3: Due diligence and selection
After narrowing the shortlist, conduct real due diligence:
- Visit the facility. Inspect the processes and meet the production manager, not just the sales contact.
- Review samples made to your tech pack, not generic showroom samples.
- Discuss volume commitments, pricing tiers, and lead times in writing.
This is the stage where most apparel brands lose money quietly. A factory that looks right on a spec sheet can be wrong for your style complexity, your minimums, or your reorder cadence.
Step 4: Negotiating the contract
A proper contract is not a one-page purchase order. It covers:
- Product specifications and the governing tech pack version.
- Quality control measures and compliance standards.
- Intellectual property rights and confidentiality.
- Payment terms, including deposits, balance on shipment, and penalty clauses for late delivery.
- Dispute resolution and governing law.
Step 5: Prototype and trial production
Before full-scale production, the factory produces a sample or a small trial batch. This stage exists to:
- Test the product under actual production conditions, not sample-room conditions.
- Adjust the design, materials, or construction based on what the trial exposes.
- Confirm the finished product will meet specification before you commit the full PO.
Skipping this step is the single most common root cause of a bulk rejection.
Step 6: Full-scale production
Once the prototype is approved, the bulk PO goes into production. During this phase the factory:
- Adheres to the agreed timeline and quality standards.
- Provides regular WIP updates, ideally per PO, per style, per color.
- Flags material shortages or sub-supplier delays early.
This is where PO-level visibility matters most. If your production team cannot see WIP against the plan, you will not learn about a delay until it is already a shipping problem.
Step 7: Quality control and testing
Quality control runs throughout production, not just at the end. Inline inspections, mid-production audits, and a final pre-shipment inspection should all be in the contract. The goal is to catch defects while the line is still running, not after goods have crossed an ocean.
Step 8: Shipping and logistics
After production, the factory handles shipping to the brand’s warehouse, 3PL, or in some cases directly to a key wholesale account. This includes:
- Proper packaging for transit, with carton labels that match your WMS or 3PL receiving template.
- Customs and import/export documentation.
- Coordination with freight forwarders.
The handoff from factory to warehouse is the stitch point where inventory truth either holds or breaks. If the ASN does not match the physical cartons, the receiving team will spend days reconciling, and your available-to-sell numbers will be wrong for the entire window.
What are the real advantages of contract manufacturing?
Cost efficiency. Contract manufacturing cuts capital expenditure. You do not buy sewing machines, lease a factory, or train operators. In regions with lower labor costs, unit economics improve further. For a brand in the $10M to $30M range, this is often the difference between a viable margin and no margin.
Focus on core competencies. Outsourcing production frees internal resources for design, merchandising, wholesale sales, and DTC marketing. These are the activities that actually build brand equity. Running a factory does not.
Scalability. Contract manufacturers can flex production up or down with demand. A brand with a hit style can reorder without building a second line. A brand with a slow season does not carry idle factory overhead.
Access to expertise and advanced equipment. Specialized factories invest in machinery and process knowledge that a single brand could not justify alone. Partnering with them gives you access to technique and technology without the capex.
Expansion into new markets. Factories located near target markets can shorten lead times and reduce landed cost. A brand selling in Europe may benefit from Portuguese or Turkish production. A brand focused on North America may use Mexican factories to shorten the sea leg.
What are the real disadvantages, and when does contract manufacturing stop working?
Quality control issues. When a third party owns the line, direct oversight is harder. Differences in quality standards, operator skill, and inspection discipline can produce defects that reach the warehouse. Once a bad shipment hits a wholesale DC, it can trigger chargebacks that erase the margin on the whole PO.
Intellectual property risk. Outsourcing exposes your tech packs, patterns, and sometimes your sales data to third parties. In jurisdictions where IP enforcement is weak, this risk is material. It is not theoretical.
Dependency and loss of control. If one factory produces 60 percent of your SKUs and misses a delivery, your entire season moves. High concentration is a strategic vulnerability. The fix is a second qualified supplier for critical categories, not just a backup on paper.
Communication and cultural barriers. Contract manufacturing often crosses languages and time zones. Miscommunications cause missed deadlines and wrong materials. To reduce friction, teams increasingly use tools like Google Meet transcription to keep a shared written record of what was agreed in each call.
Long lead times. Overseas production usually means 90 to 150 day lead times from fabric commit to warehouse receipt. That cadence makes trend-chasing nearly impossible and forces earlier buy decisions, which raises forecast risk.
Hidden costs. Freight, duties, customs clearance, sampling, failed inspections, and reworks all add to the headline unit price. The quoted FOB cost is rarely the landed cost. Brands that do not track landed cost per unit tend to overestimate gross margin by several points.
When should an apparel brand use contract manufacturing versus in-house production?
The honest answer: almost every apparel brand under $100M should be using contract manufacturing for the bulk of production. In-house production only makes sense when the construction is proprietary, the volume is unpredictable in a way that penalizes long lead times, or the brand story depends on vertical integration (made-in-city positioning, for example).
For everyone else, the question is not whether to outsource. It is how to structure the outsourcing so the operational cost does not eat the unit-cost savings. That is where the 6 Breakpoints framework becomes useful.
How does contract manufacturing create the 6 Breakpoints, and how do you contain them?
Contract manufacturing touches at least four of the 6 Breakpoints of Apparel Operations directly.
Breakpoint 1: Product data fragments. The tech pack lives in one place, the costing lives in another, the PO sits in email, and the factory works from a slightly older version. Every version drift becomes a quality issue in bulk. The containment is a single source of truth for product data (a PIM or PLM) that the factory references by version number.
Breakpoint 2: Production and supply execution drift from the plan. Without PO-level WIP visibility, delays are invisible until the ship date is already missed. The containment is a production module that tracks each PO against planned milestones (fabric in, cutting, sewing, finishing, packed, shipped) with factory updates against each stage.
Breakpoint 3: Inventory truth gets weaker. When factory ASNs do not match physical cartons, receiving reconciliation can take days and available-to-sell is wrong during that window. The containment is a tight ASN-to-receipt workflow in the warehouse, with mismatch exceptions flagged in real time.
Breakpoint 4: Order flow becomes harder to trust. If finished-goods arrival dates slip, wholesale orders cancel and DTC backorders accumulate. The containment is linking production dates to the order book, so sales and customer service see the same expected availability as planning.
This is the operational case for a unified apparel operations platform. Uphance exists to hold product data, production, inventory, and orders on the same spine, so a contract manufacturing shift propagates to every downstream team automatically.
How do you choose and manage a contract manufacturer well?
1. Vet the factory against your actual product
Samples made to your tech pack reveal more than any audit score. Ask for a sample at your true complexity, not a showroom piece.
2. Check capacity, compliance, and cultural fit
Confirm the factory has slack in the months you need it, holds the certifications your wholesale accounts require, and communicates in a cadence you can live with.
3. Define expectations in writing
Agree on tech pack version control, defect tolerances, inspection standards (AQL levels), shipment windows, and penalty clauses. Vagueness here guarantees a dispute later.
4. Establish a strong contract
The contract should cover product specifications and quality requirements, intellectual property rights, confidentiality, compliance with laws, pricing and payment terms, and dispute resolution mechanisms.
5. Implement your own quality control
Do not rely on the factory’s internal QC alone. Use a third-party inspection service for inline and pre-shipment inspections on every meaningful PO. The cost is small compared to a chargeback.
6. Keep communication open
Regular standing calls, weekly WIP reports, and site visits when stakes are high. Shared written records of every agreement.
7. Plan logistics properly
Know the lead times, shipping lanes, customs regimes, and landed cost per unit for each sourcing region. Build the duty and freight into your costing before you set wholesale and retail prices.
8. Evaluate and evolve
Review supplier performance quarterly on quality, on-time delivery, and responsiveness. Replace factories that consistently miss, and reward factories that hit.
What this means for an apparel operations team
Contract manufacturing is not the risk. Running contract manufacturing on spreadsheets and email is the risk. If your design team ships a tech pack, your production team cuts a PO, your warehouse team receives the carton, and your sales team quotes availability, those four handoffs have to run on the same data. When they do not, every advantage of outsourcing (lower unit cost, faster scaling, access to specialized machinery) gets consumed by reconciliation work, cancelled wholesale orders, and chargebacks.
The practical fix is boring and effective. Version-controlled tech packs. PO-level WIP visibility. Inbound inspection at the warehouse. Landed cost per unit tracked on every receipt. A production calendar that the sales team can see. Done well, contract manufacturing is the operating model that lets a $5M brand grow into a $50M brand without building a factory. Done badly, it is the reason that same brand misses its spring delivery and spends the summer apologizing to buyers.
Frequently asked questions
Where this fits in the Uphance platform
Ruchit writes about product strategy for apparel operations, covering how mid-market fashion brands use connected workflows to manage product development, inventory, orders, warehouse execution, and reporting. As Head of Product at Uphance, he shapes the roadmap that ties PLM, PIM, BOM management, allocation, fulfillment, and warehouse operations into one system. His articles dig into apparel-specific operational mechanics: tech packs, spec sheets, putaway, pick-pack, landed cost, and the data plumbing that makes inventory truth possible across multiple channels and locations. He focuses on the workflow-level questions that separate generic ERPs from systems built for how apparel brands actually run.
Ronnell writes about onboarding, adoption, and operational readiness for apparel brands moving to a connected platform. His articles focus on what it takes to go live with confidence and sustain strong execution across channels, warehouses, and teams. As Head of Customer Success and Onboarding at Uphance, he leads the implementation phases that turn a software signature into running operations. He writes about kickoff scoping, data migration, sandbox cutover, change management patterns, and the stakeholder alignment work that determines whether a connected platform actually changes how a brand runs, or just adds another login to the existing chaos.