Pre-production sample approval sequence: six gates before bulk cut
What is a pre production sample approval sequence and why do six gates matter?
It is Tuesday afternoon in a merchandising office and the production manager is on WhatsApp with a factory in Tiruppur. The factory wants cut approval on 4,200 units of a jersey dress by end of day so they can hold their fabric booking. The fit sample landed last week and the designer approved the silhouette. Nobody has seen a size set. The lab dip for the second colorway is still with the mill. The care label wording changed three days ago and nobody told the trims supplier. The production manager approves the cut anyway because the ship window is fixed and the alternative is a two week slip. Six weeks later, 1,100 units arrive with the wrong care label and a graded fit that breaks at size XL. The rework bill lands in finance and nobody can reconstruct which gate got skipped.
A pre production sample approval sequence is the ordered protocol of six sampling gates a style must clear before a factory is authorized to cut bulk fabric. The gates are proto sample, fit sample, size set, pre-production sample (PP sample), top of production sample (TOP), and shipment sample. Each gate answers a distinct question, produces a specific artifact, and has a named approver. The sequence is not a suggestion. It is the mechanism that keeps bulk production faithful to the tech pack, and it maps directly onto BP2 of the 6 Breakpoints framework, where production execution starts drifting from the plan the moment sampling discipline breaks.
Why does the sequence break in the first place?
From the evaluation calls I sit in on with apparel brands in the $10M to $30M band, the same pattern shows up. The brand has a PLM or a shared drive with tech packs. The designer approves fit off a video call. The production manager greenlights bulk on a WhatsApp thread. There is no single record of what was approved, by whom, against which version of the tech pack, on what date. When a defect shows up in bulk, the reconstruction is archaeological. You are pulling screenshots from three phones, an email thread, and a Dropbox folder that has been overwritten twice.
The reason it breaks is almost never that the team does not know the gates exist. Design and production teams inside the ICP know their craft. It breaks because the calendar pressure of a fixed retail float date, combined with a factory holding capacity, makes gate-skipping feel rational in the moment. The proto is late so you compress fit. Fit is late so you skip size set and go straight to PP. PP is late so you approve bulk off a photograph of the PP sample rather than the sample itself. Every compression is a rational decision. Cumulatively they guarantee bulk arrives wrong.
The honest position: gate compression is a symptom of a critical path that was never load-bearing. If your time and action calendar is a spreadsheet that gets updated on Fridays, it is not a critical path. It is a report. A real critical path refuses to let a style progress until the prior milestone is stamped as complete, with the approving name and the version of the tech pack it was approved against.
Gate 1: what does the proto sample actually prove?
The proto is the first physical translation of the sketch. It uses whatever fabric is on the factory shelf, whatever trims are lying around, and it exists to answer one question: does the silhouette work in three dimensions the way it worked on the illustration. Approving a proto is approving the design intent, not the specs, not the color, not the construction.
The common mistake is asking the proto to do the work of the fit sample. Designers see a proto in the wrong fabric and start red-lining seam allowances. That feedback is premature and it confuses the factory. A clean proto gate produces one artifact: a signed decision that the silhouette is approved to proceed to fit, with any silhouette-level changes documented against the tech pack. The construction detail comes later.
If the proto is being built directly from an Illustrator flat that has been synced into the tech pack via a live two-way plugin rather than emailed as a PDF, you have already reduced one class of drift, which is the designer’s flat and the factory’s flat disagreeing about a dart placement. This is where PLM tooling earns its keep, not in the folders and permissions, but in the round-trip fidelity between design and the tech pack.
Gate 2: what is the fit sample supposed to test?
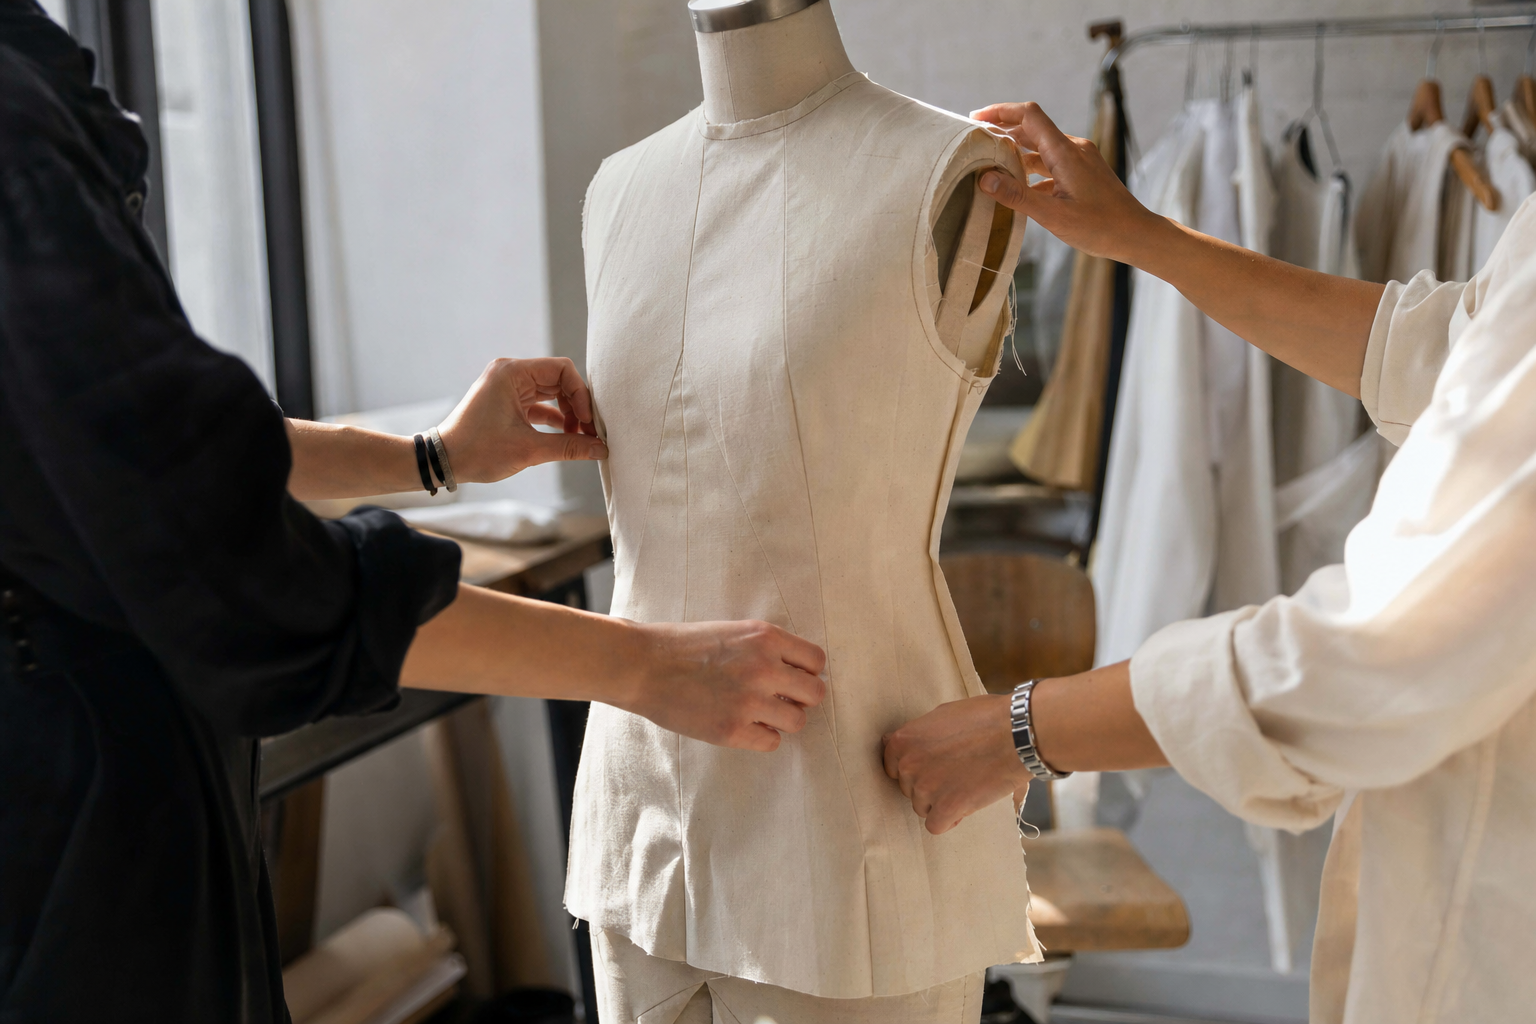
The fit sample is made in the actual bulk fabric, or the closest available substitute, at the base size. It is fitted on a live model or a form matched to the brand’s grade rule. The question it answers is whether the tech pack measurements produce the fit the brand intends on the body it intends to fit.
Fit approval is where most brands under-invest. A single fit session with a designer and a production manager in the room, judging by eye, is not a fit approval. A defensible fit gate produces measurements taken at the points of measure listed in the tech pack, deltas against tolerance, photographs from four angles, and a signed decision that specifies whether the tech pack numbers stand or which numbers change and by how much.
The rule I would defend: no style advances past fit until the measurement chart is either confirmed or revised in writing against the tech pack version number. Verbal fit approval is not approval. It is a memory that will not survive the next fit meeting on a different style.
Gate 3: why does size set matter more than teams think?
Size set is the gate everyone wants to skip. It costs money, adds two to three weeks, and feels redundant if fit was clean. Skipping it is where brands find out at retail that their XL breaks at the armhole and their XS drowns the model.
Size set produces one sample per size in the size run, made off the approved fit sample’s specs, graded per the brand’s grade rules. You are testing whether the grade holds across the range, whether points of measure that were fine at the base size become wrong at the extremes, and whether the fabric behaves consistently across cutting layouts. For any style with meaningful stretch, drape, or bias content, the grade often does not hold linearly. You find that at size set or you find it in customer returns.
My point of view: size set is non-negotiable for any style shipping to wholesale accounts with size compliance clauses, and for any DTC style where the return rate on a prior season for that silhouette was above ten percent. If the finance team pushes back on the sample cost, price the alternative, which is a bulk order graded wrong across 15 percent of the range.
Gate 4: what does the PP sample actually authorize?
The pre-production sample is the final construction proof. It is made in bulk fabric, with bulk trims, at the correct color, on the same line and machinery that will run bulk. Its purpose is to prove that every element the factory will use in bulk actually works together. This is the last gate before cut authorization.
A PP sample approval covers construction, stitching type and SPI at every seam, trim placement, label placement and wording, care label content, fiber content statement, country of origin, hangtag configuration, and packaging method. If any of these is unresolved at PP, the gate does not close. The compression that kills brands is approving PP with an open item, on the understanding that the factory will fix it in bulk. Factories do not fix it in bulk. They run bulk with whatever is on the floor.
The PP sample is where the production drift diagnostic either does its job or reveals it was never wired in. If your system cannot show, at any moment, which styles are past PP approval and which are not, your bulk authorizations are running on trust rather than on record.
Gate 5: what changes at top of production?
Top of production sample is pulled from the first cut and sewn units off the actual bulk run. It is not a separate sample made to different rules. It is a random pull from the first fifty or so pieces off the line. Its purpose is to verify that what the factory is actually producing matches what was approved at PP.
TOP catches the drift between an approved PP sample and a factory that has forgotten which trim was approved, or has swapped the thread color because they ran out, or has used a different needle size that puckers the seam on lightweight fabric. TOP approval either confirms bulk continues, or it stops the line. Stopping the line at TOP is expensive. Not stopping the line and shipping wrong bulk is more expensive, and the cost shows up two months later as retailer chargebacks or DTC returns.
The operational discipline that separates competent production teams from the rest: TOP is inspected against a physical PP sample retained by the brand, not against a photograph. If your PP samples are not archived and retrievable, TOP inspection is theatre.
Gate 6: what is the shipment sample and who signs it?
The shipment sample is pulled from finished, packed inventory before it leaves the factory floor. It confirms that the units in the carton match the units in the TOP sample, that packaging is correct, that polybag labeling matches the PO, and that carton content matches the packing list. For wholesale-bound goods, it is also the final check that retailer-specific compliance requirements, hangtag placement, price tickets, pre-ticketing, GS1-128 carton labels, are actually on the units and cartons that will ship.
Shipment sample approval is often owned by QA or the compliance lead, not the production manager. That handoff matters because the person who has spent six months getting the style to this point has a bias toward shipping. The person doing final compliance inspection needs to be structurally allowed to hold a shipment.
For a brand like Magnolia Pearl running drops with international duties and same-day fulfillment expectations, shipment sample discipline is what protects the promise made to the customer. A drop that ships with the wrong hangtag is a customer service problem for weeks. A drop that ships with the wrong care label content is a regulatory problem in the EU.
Where does the sequence live operationally?
The sequence lives in three places at once. It lives in the tech pack, which is the source of truth for what each gate is measuring against. It lives in the critical path, which is the calendar that refuses to advance a style until the prior gate closed. And it lives in the sample tracker, which is the record of which sample of which style is currently where, with which approver, and how many days late against plan.
Brands running this on spreadsheets and Dropbox typically lose 6 to 9 hours per week reconciling which sample is where, and that is before any of the reconciliation work at the inventory and order end of the business. For the $15M brand running wholesale plus DTC plus a 3PL, the sampling reconciliation stacks on top of the inventory reconciliation and the order reconciliation, and the aggregate is one full time person doing data plumbing rather than operations work.
The fix is architectural. It is a PLM with a live tech pack, a critical path calendar that flags slippage automatically, and sample status that updates as gates close, all in the same system as production orders so that cut authorization is a downstream event from PP approval rather than a parallel conversation on WhatsApp. This is where connected apparel operations either exist or do not. There is no middle ground where sampling lives in one tool, production in another, and reconciliation is a weekly meeting.
What does gate discipline cost you when you get it wrong?
Run the arithmetic on a single style that skipped size set and shipped bulk with a grade break at XL. Assume 3,000 units, 20 percent in the affected sizes, so 600 units suspect. Assume 40 percent of those require rework or markdown, so 240 units at an average cost impact of $18 per unit between rework labor, shipping, and margin loss. That is $4,320 on one style. Multiply by the number of styles that skipped size set in a season, and the number is not small.
Run it again for a PP sample approved with an open trim item. Bulk arrives with the wrong care label content. In the EU, you are relabeling. Relabel cost per unit lands between $2 and $4 depending on volume and location. On a 5,000 unit order, that is $10,000 to $20,000, plus the delay to the ship window, plus the retailer chargeback if the ship window slips past the cancel date.
These are not catastrophic numbers on any single style. They are the reason gross margin erodes half a point per season without anyone being able to point at what caused it. Gate discipline is a margin protection instrument. It is not a design luxury.
The signal that tells you your sequence is broken
If your production manager cannot tell you, in under sixty seconds, which styles in the current season are past PP approval and which are not, your sequence is broken. If your critical path is a spreadsheet updated weekly rather than a live calendar with automatic slippage flags, your sequence is broken. If bulk cut authorizations happen over WhatsApp rather than as a system event triggered by PP closure, your sequence is broken.
None of this is about tooling for its own sake. It is about whether the brand can honor the ship windows it has already committed to, at the quality the customer has already paid for, without absorbing the margin cost of avoidable rework. The six gates are the mechanism. The critical path is the enforcement. The tech pack is the reference. When those three are wired into the same system, sampling stops being a source of drift and becomes the thing that prevents it.
Where is your operation on the 6 Breakpoints curve?
The assessment scores your apparel operation across all six breakpoints (product data, production, inventory truth, order flow, warehouse execution, reporting) and identifies which one is hurting you most.
Frequently asked questions
Shubham writes about evaluating ERP fit, assessing operational complexity, and how apparel brands can tell whether their current systems are helping or holding them back. As a Solutions Consultant at Uphance, he runs discovery conversations and fit assessments for apparel brands moving off patchwork stacks of PLM, PIM, inventory, and B2B tools. His articles cover ERP selection, vendor RFPs, comparison frameworks, and the operational signals that tell a brand it has outgrown spreadsheets and point solutions. He focuses on how mid-market apparel teams evaluate connected platforms against the cost of staying with what they have.
Ruchit writes about product strategy for apparel operations, covering how mid-market fashion brands use connected workflows to manage product development, inventory, orders, warehouse execution, and reporting. As Head of Product at Uphance, he shapes the roadmap that ties PLM, PIM, BOM management, allocation, fulfillment, and warehouse operations into one system. His articles dig into apparel-specific operational mechanics: tech packs, spec sheets, putaway, pick-pack, landed cost, and the data plumbing that makes inventory truth possible across multiple channels and locations. He focuses on the workflow-level questions that separate generic ERPs from systems built for how apparel brands actually run.